• +1 954 484 9700 Talk to an expert
  • 4180 NW 10 Avenue Ft. Lauderdale, FL-US

CASE STUDY

Automated Adhesive Spray for High-Speed Tissue Converting

A Fortune 100 consumer products manufacturer was fighting adhesive problems at three points on its high-speed tissue converting lines — and paying for them in rejects, downtime, and wasted material. Spraymation replaced a patchwork of aging equipment from three vendors with one unified, multi-station adhesive spray system. Within 90 days, the manufacturer documented a 99.7% tail seal first-pass rate, a 40% reduction in adhesive consumption, and a 12% increase in converting line speed.

Results at a glance

40%

Reduction in adhesive consumption

99.7%

Tail seal first-pass rate

<1 Year

Payback period

12%

Increase in line speed

Project Overview

Industry

Tissue & Towel Converting

Application

Tail Tie, Core Pickup & Ply Bonding

Product

Bath Tissue & Paper Towel Rolls

Coating

PVA & Hot Melt Adhesive

The Challenge

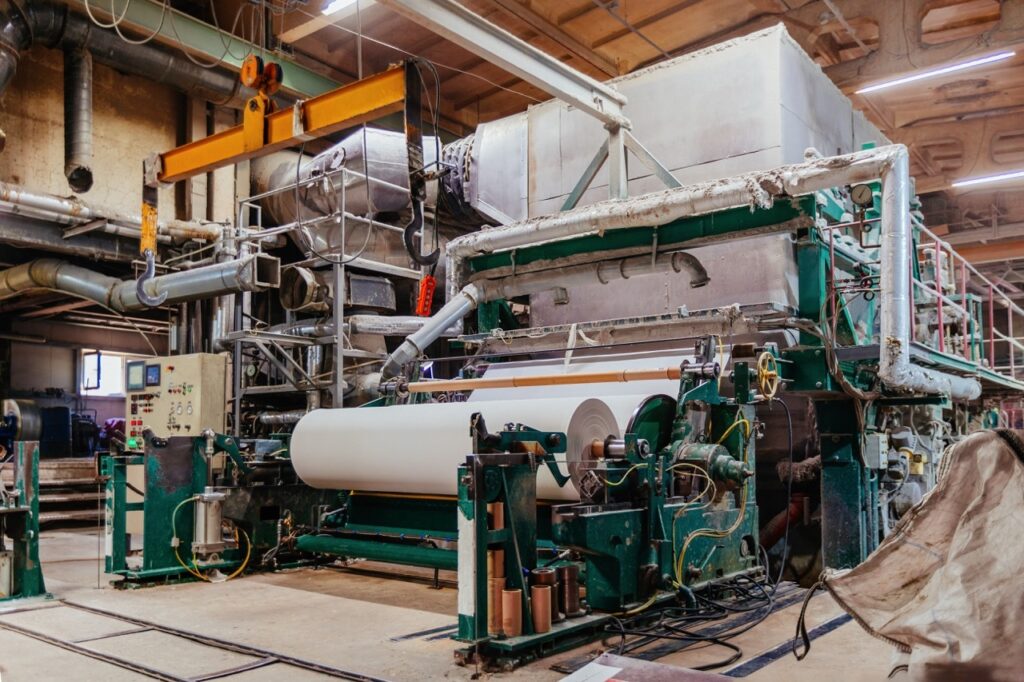
Three adhesive applications run simultaneously on a modern tissue converting line: tail tie (sealing the outer sheet to the finished roll), core pickup (bonding the leading edge of the web to the cardboard core), and ply bonding (laminating multiple plies together). At line speeds exceeding 2,000 feet per minute, every one must perform flawlessly on every roll.

The manufacturer’s existing spray equipment — a mix of aging applicators from multiple vendors — was creating compounding problems across the converting operation:

[01]

Inconsistent tail tie seal.

The tail seal is the first thing a consumer sees when they pick up a roll. Uneven adhesive beads left tails that flagged open during packaging, stacking, and shelf handling — triggering automatic rejects at the packaging line and driving consumer complaints on rolls that slipped through.

[02]

Core pickup failures.

Inconsistent spray at the core station meant the leading edge of the web occasionally failed to bond at startup. Each missed pickup forced the line to slow or stop, re-thread, and restart — several minutes of lost production per occurrence, across hundreds of events per month.

[03]

Over-application and soak-through.

Without precision flow control, operators ran adhesive flow high to compensate for inconsistent spray. Excess adhesive soaked through sheet layers, creating wet spots and stiff patches — and on premium SKUs, driving downgrades to lower-tier product at reduced margin.

[04]

Excessive waste and cleanup.

Overspray and dripping from worn applicators contaminated the line, consuming maintenance labor, causing unplanned downtime, and degrading embossing roller pattern quality.

[05]

Multi-vendor complexity.

Equipment from three suppliers meant incompatible controls, separate spare parts inventories, and no single-source accountability. Troubleshooting a tail tie defect required diagnosing across multiple vendors’ hardware.

The Spraymation Solution

Spraymation engineered a unified, multi-station adhesive spray system covering all three application points under a single integrated control architecture.

Key System Components

Precision spray applicators for tail tie — Electrically-actuated spray applicators cycle at high speed, synchronized to the converting line’s cut-off frequency, applying a narrow, uniform adhesive bead only to the designated tail zone — a clean seal with no soak-through to inner sheets.

Core pickup spray station — Dedicated nozzles apply a precise adhesive line to the core surface, timed to web pickup. Closed-loop control linked to the rewinder’s encoder signal keeps placement accurate through acceleration and deceleration cycles.

Ply bonding with metered slot coaters — Slot coaters with metering pumps apply a thin, uniform adhesive film between plies across the full web width — eliminating the over-application behind stiff spots and visible adhesive marks.

Unified programmable control — All three stations run from a single Spraymation controller with touchscreen HMI and recipe storage for every SKU — single-ply or double-ply, standard or premium, towel or tissue. Line speed compensation is automatic across all stations.
Heated fluid delivery with filtration — Heated supply lines hold consistent adhesive viscosity from tank to nozzle for both PVA and hot melt, while inline filtration prevents nozzle clogging from paper dust — a persistent problem in converting environments.

Engineering Approach

Spraymation’s engineering team spent three days on-site mapping the line’s geometry, speed profile, adhesive types, and SKU matrix. Nozzle selection and spray pattern geometry were validated at Spraymation’s Fort Lauderdale facility using the manufacturer’s actual adhesive grades and web samples. The complete system was assembled, wired, and factory acceptance tested before shipment — and installed during a scheduled weekend maintenance window with no unplanned production downtime.

The Results

Within 90 days of commissioning, the manufacturer documented:

99.7%

Tail seal first-pass rate.

Tail flagging was virtually eliminated. Automatic rejects at the packaging line fell by more than 95%, and open-tail consumer complaints dropped to near zero.

40%

Reduction in adhesive consumption.

Metered delivery and closed-loop flow control ended chronic over-application across all three stations — a substantial annual material savings at the manufacturer’s adhesive volumes.

12%

Increase in converting line speed.

Fewer core pickup failures and cleaning stoppages let the line run at higher sustained speed — additional cases per shift with no new converting equipment.

Single-source accountability.

One Spraymation system replaced three vendors’ equipment. Spare parts consolidated, maintenance simplified, and mean time to resolution for spray defects dropped from hours to minutes.

<12 mo

Payback period.

Combined savings in adhesive, scrap, throughput, and maintenance labor returned the full system investment within the first year.

Why Spraymation

65+ years of spray automation expertise

Full in-house engineering and fabrication

Serves Fortune 100 tissue and hygiene manufacturers

Factory acceptance tested before shipment

Get Started

Ready to Discuss Your Application?

Whether you’re fighting tail tie failures, core pickup misses, or adhesive waste on your converting line, Spraymation’s engineers can design a system around your exact line geometry, speeds, and adhesives — and prove it out before it ships.

Case Study CS-2026-TC-001 | © Spraymation Holdings Inc. 2026 | ISO 9001:2015 Certified

Secret Link